What Can a 40-Ton 1600mm Electric Press Brake Bend?
Table of Content
When selecting and using a press brake, three practical questions come up again and again:
1. How do I choose the right press brake for my workpieces?
2. Once I have selected a machine, how do I know what it can reasonably bend?
3. If I need to bend many different workpieces, how should I choose the lower die?
In this article, we use a real 40T / 1600 mm servo electric press brake project to answer all three—from the customer’s expected workpiece range to the final machine working range and tooling configuration.
For a broader overview of machine type, tonnage and configuration, see our Press Brake Selection Guide.
1. How Do You Select the Right Press Brake?
A common question when selecting a press brake is:
Should I buy 40T, 60T or 100T?
A better starting point is not the machine, but the workpiece.
For air bending, the required bending force is mainly determined by:
Material + Thickness + Bending Length + V-Die Opening
Once these conditions are known, the required tonnage can be calculated using our Press Brake Tonnage Calculator and used as the basis for machine selection.
This is also why questions such as “Can a 40-ton press brake bend 4 mm steel?” cannot be answered by thickness alone. Change the material, bending length or V opening, and the required force changes as well.
Starting with the Customer’s Expected Workpieces
In this project, the customer planned to use the machine for different sheet-metal fabrication jobs rather than one fixed product.
The expected work covered aluminum, mild steel and stainless steel, with different thicknesses and bending lengths.
We therefore started with the normal selection process: calculate the required bending force from the expected workpieces before deciding on the machine.
Initial Bending Requirements
| Aluminium | |||
| Thickness | Length to bend | Recomended V | Tonnage |
| 2-3mm | 1600mm | 12 | 31.2 |
| 4mm | 1600mm | 24 | 41.6 |
| 5mm | 1600mm | 32 | 52 |
| 6mm | 1000mm | 48 | 39 |
| 8mm | 600mm | 64 | 31.2 |
| Mild Steel | |||
| Thickness | Length to bend | ||
| 2-3mm | 1600mm | 24 | 39 |
| 4mm | 1600mm | 32 | 52 |
| 5mm | 1000mm | 40 | 40.63 |
| Stainless Steel | |||
| Thickness | Length to bend | ||
| 2-3mm | 1600mm | 24 | 58.5 |
| 4mm | 1000mm | 32 | 48.75 |
| 5mm | 600mm | 48 | 30.47 |
The initial calculation showed that the customer’s expected work range covered significantly different tonnage requirements, with some conditions exceeding 40 tons.
If all of these conditions had been fixed production requirements, the machine would need to be selected according to those higher-load conditions.
But this was a fabrication business. The list represented the range of jobs the customer expected to encounter, rather than a fixed production schedule.
After considering the expected work range together with the application, machine size and investment, the selected machine was:
That answered the first question.
But selecting the machine created another one:
What should the practical working range of this 40-ton machine actually be?
2. Once the Machine Is Selected, What Can It Actually Bend?
A 40-ton rating tells us the nominal capacity of the machine. It does not tell us one fixed maximum sheet thickness.
The same 40-ton press brake may use its full bending length on a thinner material, while thicker or stronger materials require a shorter bending length.
So instead of defining the machine by statements such as:
“40 tons can bend X mm steel.”
it is more useful to define a working envelope based on:
Material × Thickness × Bending Length × V Opening
In other words, the first calculation helps us select the machine.
The next evaluation helps us define how the selected machine should be used.
3. So, What Can This 40T / 1600mm Press Brake Actually Bend?
For this application, we first decided to retain approximately 20% of the machine’s nominal tonnage as a capacity reserve when defining the expected working range.
For the 40-ton machine, this gave us a target calculated bending load of approximately:
≤ 32 tons
With this target established, we reviewed the customer’s expected workpieces again and adjusted the bending conditions where necessary.
The complete comparison is shown below.
Customer Requirements vs. Final 40T / 1600mm Working Range
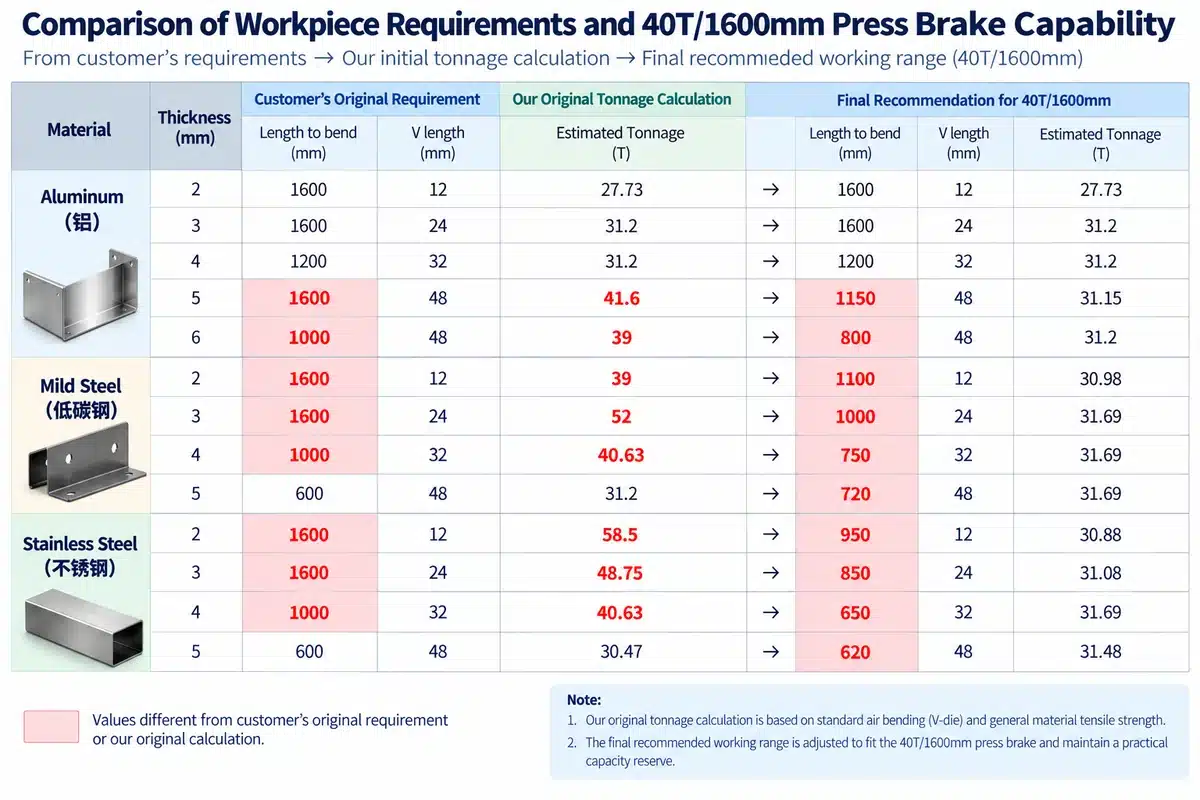
This comparison gives a much clearer answer to “What can a 40-ton press brake bend?”
Some of the original workpiece conditions already fit the defined working range, while others required a different bending length or V opening.
The important point is not any single value in the table.
It is that the capability of the machine changes with the combination of:
Material + Thickness + Bending Length + V Opening
So a 40-ton press brake is better understood through its working range, rather than by one maximum-thickness figure.
4. Why Did We Limit the Working Range to Approximately 32 Tons?
You may notice that the final recommended conditions in the table are concentrated around 32 tons or below.
This was intentional.
The 32-ton target was not calculated from the final results. It was established first.
For this particular application, we chose to retain approximately 20% of the 40-ton nominal capacity as a reserve, and then used approximately 32 tons or below as the target when defining the working range.
That distinction matters:
40T = Nominal machine capacity
≈32T = Target working load used for this application
The purpose was not to find the absolute maximum condition the machine could theoretically reach, but to define a practical range for the customer’s expected work.
The 20% reserve is specific to this application and should not be treated as a universal rule for every press brake. The appropriate working range should be evaluated according to the machine, tooling, material, bending method and actual production conditions.
5. If Many Bends Are Shorter, Why Did We Still Choose a 1600mm Machine?
The comparison table shows that some thicker or stronger materials require less than the full 1600 mm bending length.
So why not choose a shorter machine?
Because some thinner workpieces still require the full 1600 mm bending length.
This highlights an important point in press brake selection:
The thickest workpiece does not necessarily determine the required machine length.
A thicker workpiece may drive the tonnage requirement, while a longer, thinner workpiece may determine the required bending length.
That is why tonnage and machine length should be evaluated across the complete expected workpiece range rather than from one “maximum” workpiece.
For this application, 40T / 1600 mm provided the required machine length, while the working-range analysis defined how that capacity could be applied across different materials and thicknesses.
6. How Should I Choose the Lower Die for Different Workpieces?
Once the working range was defined, the required V openings were clear:
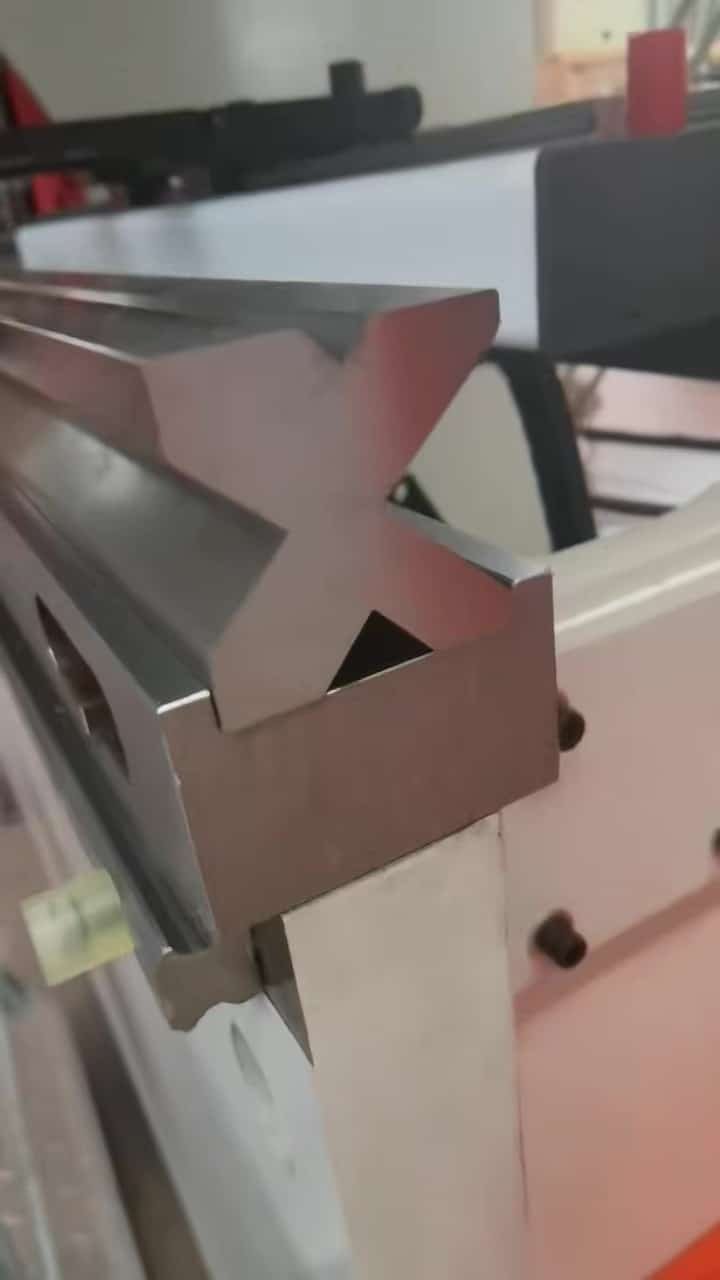
V12 / V24 / V32 / V48
Instead of using four separate lower dies, we combined these openings into one custom 4V lower die.
See more press brake tooling options